Why Default Software Material Cards Fail for Hyperelastic Rubber Simulations

Modeling Rubber and Viscoelasticity with Abaqus

Why Default Software Material Cards Fail for Hyperelastic Rubber Simulations

Every FEA engineer working with elastomers has been tempted by it at some point: you are setting up a complex assembly in Abaqus, ANSYS, or LS-DYNA, you need to model an O-ring or a vibration isolator, and there it is a built-in material library offering a pre-calibrated material card labeled simply: “Rubber (Mooney-Rivlin)” or “Neoprene.”

You click assign, hit solve, and wait.

What happens next usually falls into one of two categories:

  1. The solver fails to converge, throwing negative eigenvalues, distorted element errors, or severe volumetric locking at 15% strain.
  2. The solver converges, but the physical prototype deflects twice as much as predicted, seals leak, or the part fails in endurance testing.

Why do default material cards and generic library constants fail so spectacularly when it comes to hyperelastic materials?

The short answer: Rubber is not steel, and a generic strain energy density function is an engineering illusion.

Here is a deep dive into the physics and material realities behind why default rubber cards fail, and what you need to do instead.

1. “Rubber” Is Not a Material Specification

When you select generic Structural Steel (e.g., ASTM A36) or Aluminum 6061-T6 from a software library, the modulus and yield strength are reasonably predictable across suppliers.

Elastomers, however, are complex chemical formulations. What an engineer colloquially calls “EPDM 70 Shore A” or “NBR” is not a singular material. Its mechanical response is dictated by:

  • Polymer grade and molecular weight distribution
  • Filler loading (carbon black or silica type, particle size, and volume fraction)
  • Plasticizers and processing oils
  • Cure system (sulfur vs. peroxide vulcanization)
  • Crosslink density

Two compounds moulded to the exact same nominal durometer (e.g., 70 Shore A) can exhibit up to a 50% difference in stress-strain behaviour at moderate to large strains. Using a generic library card means you are simulating a hypothetical, chemically ambiguous rubber that likely bears zero resemblance to the compounded stock on your factory floor.

2. The Uniaxial Trap and Multiaxial Blindness

Most built-in material constants (or default fitting wizards) are calibrated exclusively against simple uniaxial tensile test data.

A hyperelastic model calibrated only on uniaxial tension is mathematically blind to other modes of deformation.

If you fit a 2-term Mooney-Rivlin or a 3-term Ogden model strictly to uniaxial data, the model might look like a perfect fit on your 2D curve. But when the FEA solver applies a triaxial or shear stress state to an element, the mathematical surface outside the uniaxial domain frequently produces unphysical behavior, including negative stiffness or severe over-stiffening.

3. The Math Behind the Crash: Drucker Stability Violations

Commercial FEA packages evaluate material stability using Drucker’s stability criterion, which requires that the work done by an incremental stress over an incremental strain must be positive. Default material cards especially higher-order polynomial models or unconstrained parameters often violate Drucker stability at strain levels just beyond the calibrated data.

When your simulation hits a strain state where the material derivative turns negative:

  1. The tangent stiffness matrix loses positive definiteness.
  2. The solver encounters material instability.
  3. The simulation diverges with a non-convergence error or localized mesh distortion.

Default cards like in Abaqus rarely warn you about the exact strain limits where their underlying coefficients become unstable.

4. Incompressibility and the Volumetric Penalty Faux Pas

Elastomers are nearly incompressible. Their bulk modulus (K) is typically 1,000 to 10,000 times larger than their shear modulus (G). Without measuring the actual bulk modulus based on proper confined volumetric testing, your contact force and groove-fill predictions are essentially guesswork.

5. Ignoring Real-World Physical Phenomena

Default hyperelastic material cards assume a conservative, frictionless, rate-independent energy potential. Real rubber, however, violates almost every assumption of pure hyperelasticity:

  1. The Mullins Effect (Stress Softening): Virgin rubber behaves stiffly on its first pull. On subsequent cycles, it softens dramatically. If your default card represents virgin data, but your actual component undergoes cyclic loading, your simulation will drastically overestimate operating stiffness.
  2. Viscoelasticity & Strain Rate Sensitivity: Default cards represent a single, unspecified strain rate. In dynamic applications (e.g., engine mounts, bump stops), rubber stiffens noticeably as frequency/strain rate increases.
  3. Permanent Set & Creep: Hyperelastic cards snap back to zero strain upon unloading with zero hysteresis loss. Real elastomeric parts exhibit residual strain and relaxation.

Summary: What Default Cards Miss

ParameterDefault Library CardReality in Physical Elastomers
Material ChemistryGeneric nominal valuesFormulations, fillers, and cure dependent
Deformation StatesTypically calibrated for 1 modeCoupled multiaxial modes (Tension, Shear, Compression, Biaxial)
Stability LimitsOften untested; prone to Drucker instabilityPhysically stable across realistic deformation ranges
Bulk ModulusArbitrary default assumptionCrucial for confined seals and contact pressure
ViscoelasticityAssumes purely elastic recoveryViscoelastic force decay and stress relaxation

The Engineer’s Checklist: Moving Beyond the Default Card

If default material cards are fundamentally unreliable, how should you simulate hyperelastic rubber accurately? Follow this workflow:

  1. Test Your Specific Compound:
    Never rely on a generic handbook card for production-intent designs. Obtain physical samples vulcanized from the exact compound and process used in production.
  2. Characterize all Deformation Modes:
    • Uniaxial Tension
    • Equibiaxial Tension
    • Unaxial Compression
    • Planar Shear
    • Volumetric Compression
  3. Select the Right Potential for Your Strain Range:
    • Strains: Less than 30-50%: Neo-Hookean or Mooney-Rivlin
    • Strains up to 150-200% Yeoh (reduced polynomial) or Arruda-Boyce
    • Strains Greater than 300%, High Non-linearity: Ogden (3-term or higher)
  4. Run Single Element Checks:
    Before running your component model, run your fitted coefficients through the software’s built-in stability evaluator across all deformation modes up to the maximum expected strain.
  5. Use Hybrid / Mixed-Formulation Elements:
    Always pair your hyperelastic material definition with elements designed for incompressibility (e.g., Abaqus C3D8H, ANSYS KEYOPT(6)=1, or similar mixed U-P formulations) to avoid volumetric locking.

Summary

Default software material cards are useful for one thing only: sanity-checking that your boundary conditions, contacts, and solver setup execute without syntax errors.

The moment your simulation is expected to guide tooling, predict seal integrity, or assess fatigue life and durability, step away from the built-in library. In hyperelastic FEA, garbage in does not just mean garbage out, it usually means the solver won’t even run.
Engineering and Testing Challenges at Advanses

Every test we conduct at our laboratory is a real-world engineering problem. A rubber component, metal structure, polymer part, or composite assembly arrives with a failure, a performance target, or an unanswered question. The specimen has to be prepared correctly, gripped without inducing artifacts, instrumented precisely, tested under controlled conditions, and interpreted with engineering judgment grounded in mechanics and material behavior. Get any one of those wrong, and the data loses meaning.

Our FEA and durability engineering work adds another layer of complexity. A FEA simulation is only as good as the assumptions behind it. Material models have to capture real-world nonlinear behavior. Boundary conditions must represent operating reality, not idealized textbook cases. Fatigue life predictions depend on how accurately strain energy, contact mechanics, crack initiation, and load histories are understood. We routinely work on problems where a few millimeters of displacement, a small stress concentration, or a slight variation in material behavior can determine whether a component survives millions of cycles or fails prematurely in the field.

Engineering in the physical world rarely behaves perfectly. Machines drift out of calibration. Samples vary from batch to batch. Real loading conditions are seldom clean or repeatable. Components see heat, vibration, dirt, overloads, misuse, and manufacturing variations that no specification sheet fully captures. And beyond the technical complexity, we build and operate in India – where industries move at different levels of maturity, testing standards are interpreted differently across sectors, documentation can be incomplete, and engineering decisions are often made under severe cost and time pressures. This is not a limitation; it is the environment that shapes our capability. Because building reliable engineering systems in these conditions requires more than software or machinery. It requires experience, discipline, experimentation, and the ability to bridge theory with manufacturing reality. Over the years, we have built a practice that does not depend on ideal assumptions. Our strength lies in understanding how products behave in actual service conditions and helping customers make engineering decisions with confidence.

As a result, our laboratory and engineering services have become trusted partners for manufacturers, OEMs, suppliers, and product development teams across industries.

Our work supports the development and validation of components that operate in demanding environments – from automotive and industrial systems to rubber and polymer applications where durability and reliability are critical. Every project we complete strengthens not only the products we help validate, but also the engineering ecosystem that depends on accurate testing, dependable analysis, and practical problem-solving.

For more information, contact us

Advanses Non-linear FEA Solver and Material Characterization

At AdvanSES, we test polymer materials, rubber, plastics and composites. We also simulate it.

Over the past year, we’ve been building an in-house nonlinear FEA solver from the ground up in Python specifically tuned for hyperelastic and viscoelastic materials using AI. It’s in internal testing right now, and the architecture has grown into something worth sharing.

Here’s what the solver does under the hood:

>> Parsing & Model Assembly
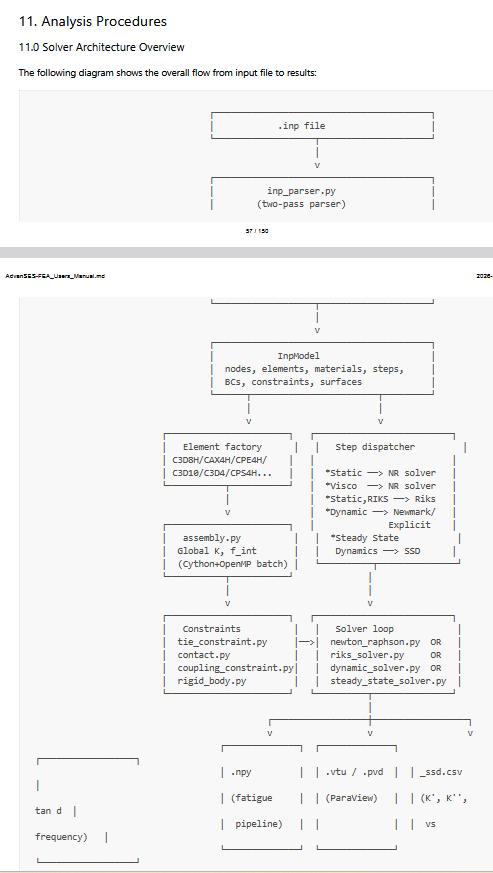
A two-pass .inp parser builds a full Inp Model of nodes, elements, materials, BCs, constraints, and surfaces, before anything is solved. Element support spans C3D8H, CAX4H, CPE4H, C3D10, C3D4, and CPS4H families. Global stiffness K and internal force f_int are assembled in Cython-accelerated, OpenMP-parallelized batches.

>> Step Dispatcher
The solver routes each analysis step to the appropriate kernel:
→ Static / Visco -> Newton-Raphson
→ Snap-through / instability -> Riks arc-length
→ Transient dynamics -> Newmark / Explicit
→ Frequency domain -> Steady-State Dynamics (SSD)

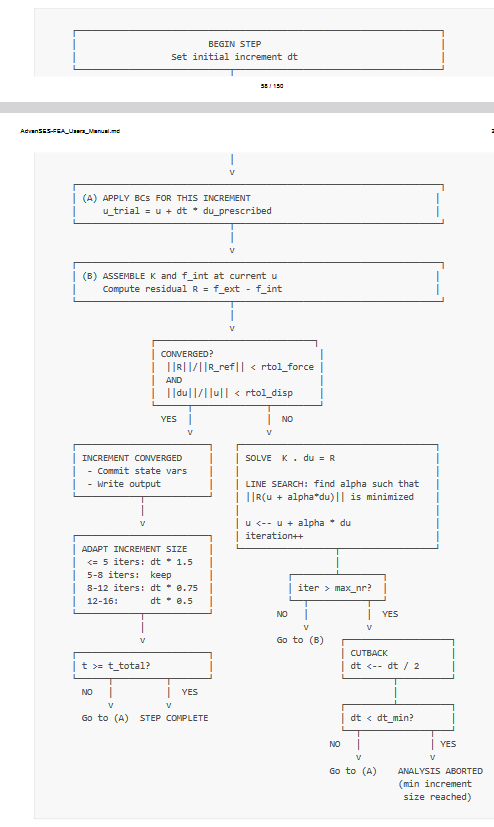
>> Newton-Raphson Loop with proper controls
This is where most solvers either earn or lose credibility. Ours implements:

  • >> Dual convergence check: force residual ||R||/||R_ref|| AND displacement correction ||du||/||u|| both must satisfy their tolerances
  • >> Line search: finds optimal step size α minimising ||R(u + α·du)||
  • >> Adaptive increment control: dt scales up (×1.5) for fast convergence, scales down (×0.75 or ×0.5) when iterations climb, and cuts back (dt/2) on non-convergence, with a hard floor dt_min before aborting

>> Outputs
Results write to .npy arrays, .vtu/.pvd for ParaView visualisation, and ssd.csv for storage modulus K’, loss modulus K”, and tan δ vs frequency which are directly usable for bushing and mount characterization reports.
A fatigue post-processing pipeline sits downstream.

Why build this instead of using a commercial solver?

Because our clients like automotive OEMs, Tier-1 suppliers, aerospace, need traceability, customization, and results that connect directly to our physical test data and short runs on components can be carried out extremely fast in a work group without waiting for a commercial solver license to be free. A solver we understand completely is a solver we can validate completely.

We’re not replacing Abaqus. We’re building the capability to run targeted, physics-correct simulations for rubber-metal bonded components like torque rod bushings, engine mounts, isolators where our test data and simulation live in the same pipeline.

If you work on NVH characterization, durability simulation, or rubber component qualification and want to talk about what tighter test-simulation integration looks like in practice I’d be glad to connect.

FEA #NonlinearFEA #RubberEngineering #ComputationalMechanics #HyperelasticMaterials #NVH #AutomotiveEngineering #AdvanSES

3-Point vs 4-Point Bend Tests on Composite Materials: Key Differences and Applications


3-Point vs 4-Point Bend Tests on Composite Materials: Key Differences and Applications

Published by: Advanses Materials Testing Laboratory | Category: Composite Materials Testing

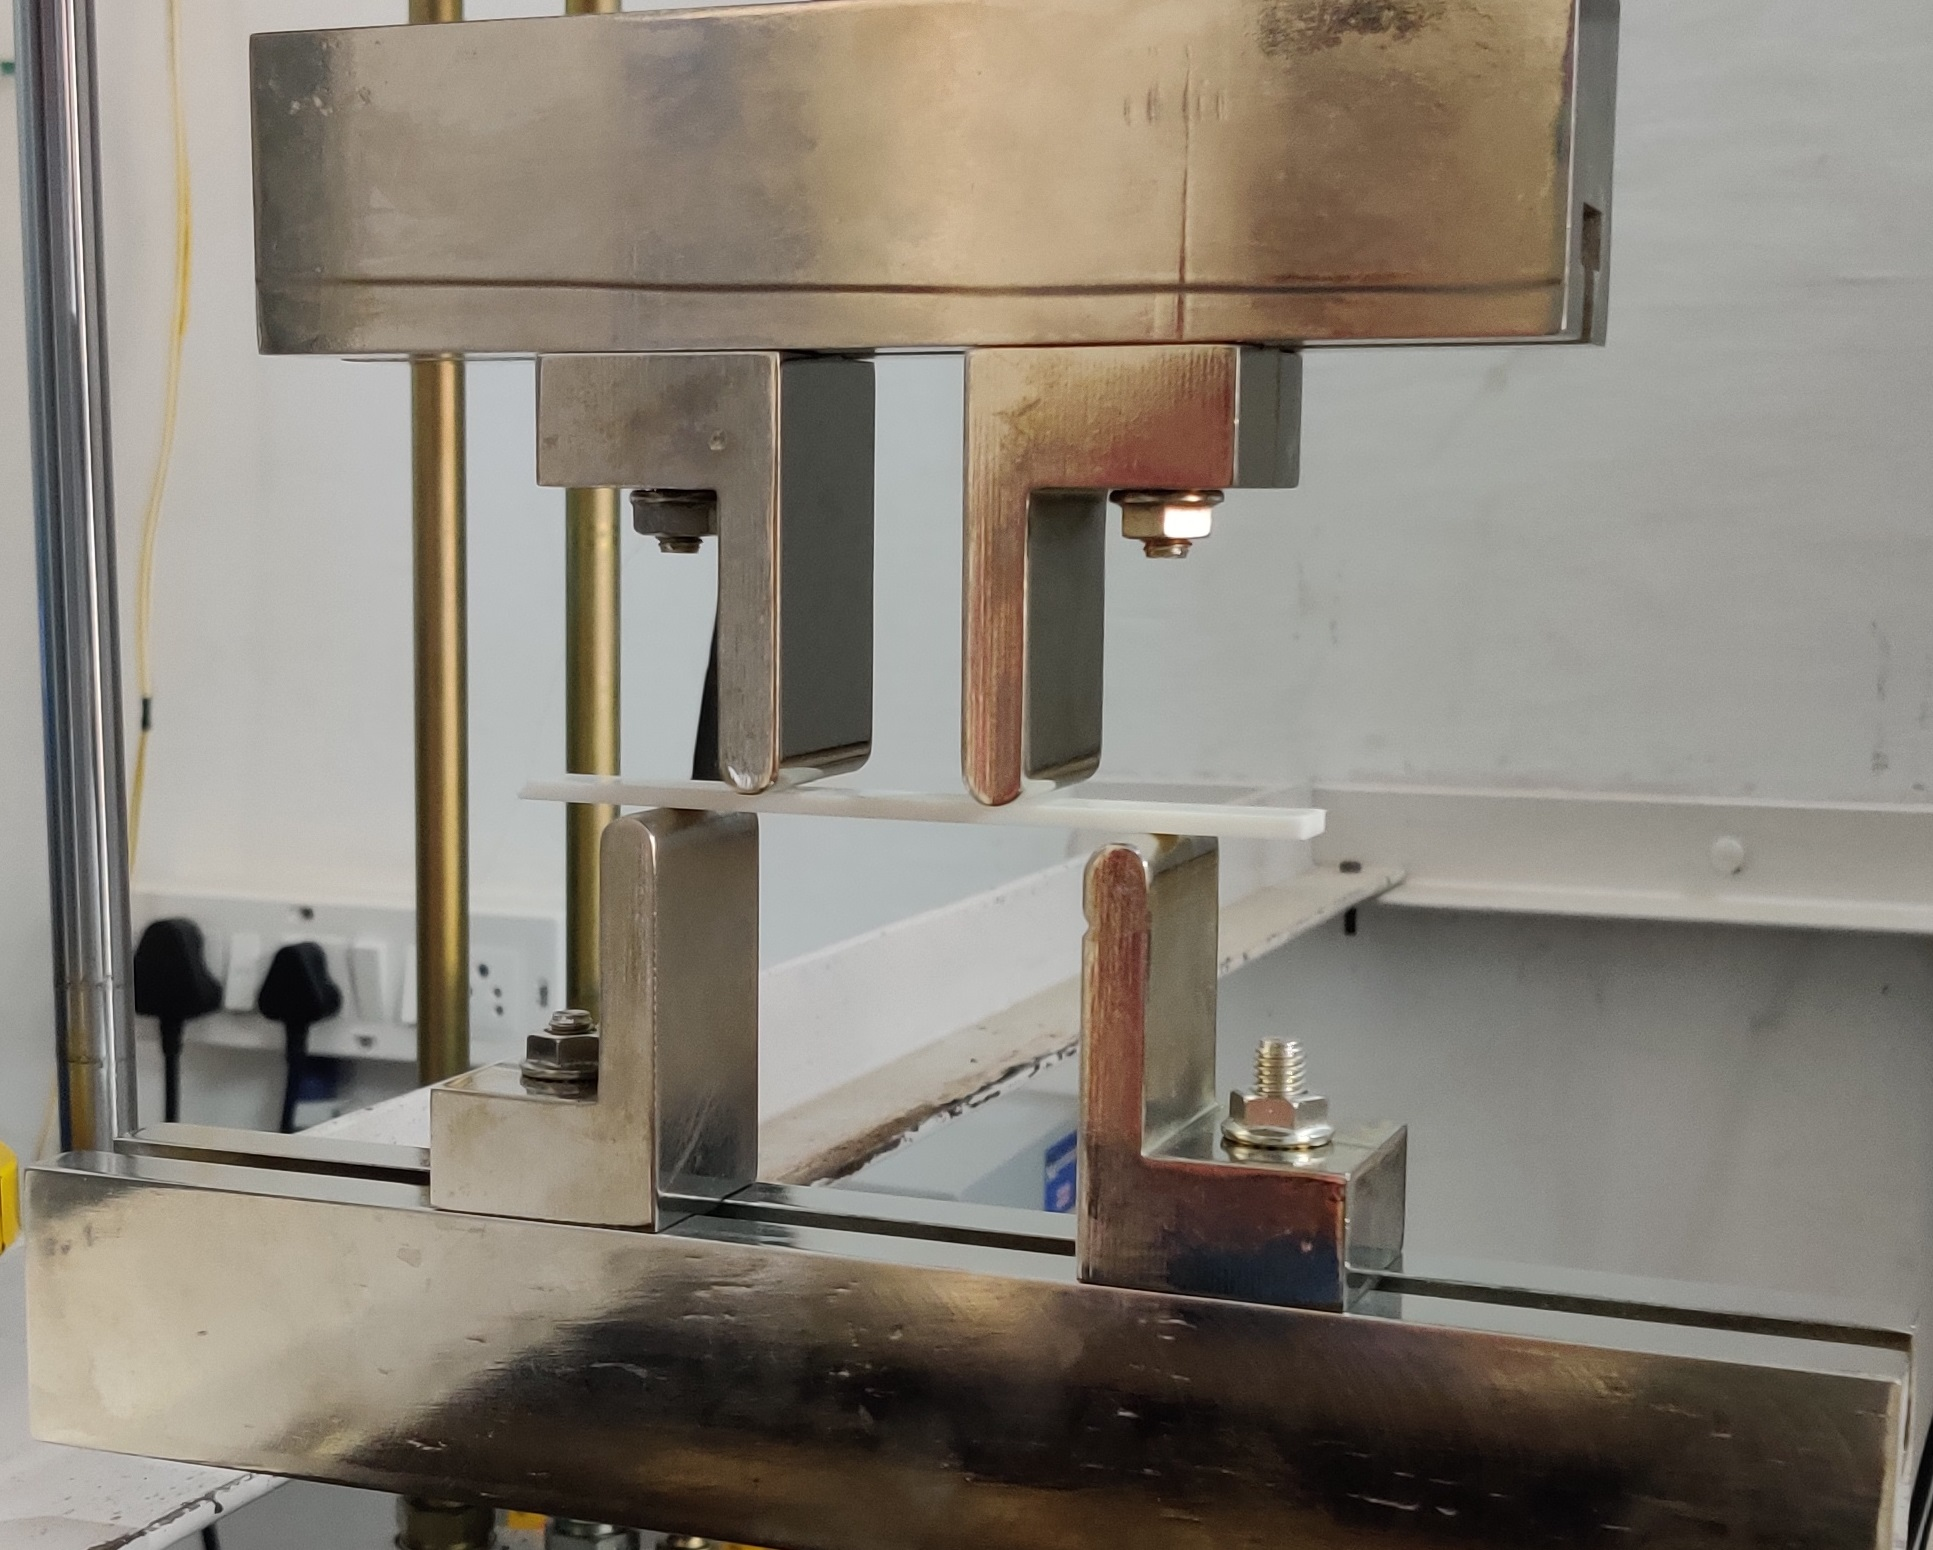
3-point and 4-point bend test on composite materials
Flexural testing setup for composite materials (ASTM D7264 / ISO 14125).

Introduction

Understanding how composite materials behave under bending loads is vital for aerospace, automotive, defense, and industrial applications. At Advanses Materials Testing Laboratory, we routinely perform 3-point and 4-point bend tests to evaluate flexural strength, stiffness, and failure behavior of fiber-reinforced composites, plastics, and advanced polymers.

Although both methods measure flexural performance, they differ in stress distribution, failure mode, and data interpretation. This article explains those differences, references key ASTM and ISO standards, and shows how engineers can use these tests for improved materials development.

What Is a Flexural (Bending) Test?

A flexural test measures a material’s resistance to bending and provides insights into:

  • Flexural Strength: Maximum stress before failure
  • Flexural Modulus: Slope in the elastic region (stiffness)
  • Flexural Strain: Deformation at break

For composites, flexural testing helps assess fiber-matrix bonding, resin quality, interlaminar strength, and laminate design integrity.

The 3-Point Bend Test

In the 3-point bend test, the specimen is supported at both ends and loaded at the midpoint by a single nose.

Relevant Standards

Test Overview

  • Support span ≈ 16× specimen thickness
  • Load applied at the center
  • Maximum stress occurs at midspan

Key Outputs

  • Flexural Strength: 3FL / (2bd²)
  • Flexural Modulus: slope of initial stress–strain curve

Advantages

  • Simple setup and quick results
  • Ideal for plastics and short-fiber composites
  • Useful for QC and production testing

Limitations

  • High stress concentration at the loading point
  • Shear and tension interaction for thicker specimens

The 4-Point Bend Test

The 4-point bend test applies load at two points, creating a constant bending moment and eliminating shear within the inner region.

Relevant Standards

Test Overview

  • Outer span ≈ 32× specimen thickness
  • Inner span = ½ of outer span
  • Constant moment region between loading points

Key Outputs

  • Flexural Strength: 3F(L₁ − L₂) / (4bd²)
  • Flexural Modulus: slope from the elastic region

Advantages

  • Produces pure bending with negligible shear
  • Better representation of laminate bending behavior
  • Ideal for advanced composites and structural validation

Limitations

  • More complex fixture setup
  • Requires precise alignment and loading

3-Point vs 4-Point Bend — Comparison Table

Feature3-Point Bend4-Point Bend
Load TypeSingle central loadTwo symmetrical loads
Stress DistributionMaximum at centerConstant between loads
Failure ModeLocalized tension/compressionUniform bending failure
Shear EffectHigherNegligible
Fixture ComplexitySimpleModerate
Applicable StandardsASTM D790 / ISO 178ASTM D7264 / ISO 14125
Best Suited ForPlastics, molded partsStructural composites
ApplicationsQC and batch testingR&D and validation

Using Flexural Test Data for Materials Development

At Advanses, we help clients transform test results into design insights:

  • Optimize Composite Layup: Compare results to identify matrix or fiber-dominated failures.
  • Assess Resin & Interlaminar Quality: Detect delamination or weak resin interfaces.
  • Correlate with Simulation: Use flexural modulus and strain data for FEA model calibration.
  • Establish Quality Benchmarks: Ensure consistent mechanical performance across production.

Choosing the Right Test for Your Application

Application TypeRecommended Test
Thermoplastics and molded parts3-Point Bend
CFRP / GFRP laminates and sandwich panels4-Point Bend
Quick QC and screening3-Point Bend
Research and structural validation4-Point Bend

Flexural Testing at Advanses

At Advanses Materials Testing Laboratory, we perform both 3-point and 4-point flexural tests in full compliance with ASTM and ISO standards. Our facilities test:

  • Polymer matrix composites (CFRP, GFRP, hybrid laminates)
  • Thermoplastic and thermoset materials
  • Reinforced plastics and filled compounds
  • Statistical data analysis and materials R&D support

We combine precision mechanical testing with data-driven materials engineering to help you design stronger, more reliable composite structures.

Contact Advanses for Flexural Testing

If you need certified testing as per ASTM D7264, ASTM D790, ISO 14125, or ISO 178 — or want to understand how flexural data can improve your product design — reach out to us today.

Request a Quote or Consultation

© 2025 Advanses Materials Testing Laboratory – Precision Testing. Reliable Results. Smarter Materials.


Mechanical Testing of Plastics, Rubbers and Composite Materials

1) Mechanical Testing of Plastics, Rubbers and Composite Materials
2) Endurance and Durability Testing
3) Dynamic Mechanical Analysis (DMA) of Materials and Components
4) Hyperelastic, Viscoelastic Material Characterization Testing
5) Data Cards for Input into FEA, CAE softwares
6) FEA Services
7) Custom Tests, NI Labview DAQ

Discover more at http://www.advanses.com

#CAE #FEA #MATERIALSTESTING #LABORATORY #ABAQUS #ANSYS #POLYMERS

Mechanical Testing of Plastics Rubbers and Composite Materials

Advanses Low Velocity Impact Testing System

The Advanses low velocity impact test system is a drop impact testing machine fully designed and developed in-house for research on composite, plastic materials. The details are as below;

  1. Force balanced all steel structure
  2. Maximum fall height of 2m.
  3. High precision loadcell of 20KN capacity
  4. Independent automatic pneumatically controlled drop system
  5. Full configurable material sample holding fixtures able to handle samples of varied sizes.
  6. High speed data acquisition system with data rate of 50,000 data samples in 1 second.
  7. All test exportable in MS Excel format.
  8. Fully benchmarked for ISO 6603 and ASTM D7136.

Advanses Low Velocity Impact Test System

Overview

The Advanses low velocity impact test system is an advanced drop impact testing machine specifically engineered for materials research. This system has been fully designed and developed in-house to provide precise testing capabilities for composite and plastic materials, ensuring reliable data for research and quality control purposes.

Key Features

Robust Construction

  • Force balanced all-steel structure ensuring stability during testing
  • Maximum fall height of 2 meters allowing for varied impact energy testing scenarios

High-Precision Measurement

  • Equipped with a high-precision 20KN capacity loadcell for accurate force measurements
  • High-speed data acquisition system capable of collecting 50,000 data samples per second

Advanced Control Systems

  • Independent automatic pneumatically controlled drop system for consistent test conditions
  • Configurable material sample holding fixtures accommodating samples of various dimensions

Data Management

  • Comprehensive test results exportable in Microsoft Excel format for easy analysis and reporting
  • User-friendly interface for efficient test setup and monitoring

Compliance

The Advanses low velocity impact test system has been fully benchmarked for compliance with international testing standards:

  • ISO 6603: Plastics — Determination of puncture impact behavior of rigid plastics
  • ASTM D7136: Standard Test Method for Measuring the Damage Resistance of a Fiber-Reinforced Polymer Matrix Composite to a Drop-Weight Impact Event

Applications

This testing system is ideal for:

  • Research and development of composite materials
  • Quality control in materials manufacturing
  • Performance testing of plastic components
  • Academic research on material impact properties
  • Product development and validation

Contact us to get the latest information and a quick quotation for all your testing needs.

How to Model Hyperelastic Materials in Abaqus: A Comprehensive Guide

Introduction

Modeling hyperelastic materials is crucial in many engineering applications, from automotive to biomedical industries. Abaqus provides powerful tools for accurately representing the complex behavior of these non-linear materials. This guide will walk you through the essential steps of modeling hyperelastic materials in Abaqus, helping you achieve more precise and reliable simulation results.

What are Hyperelastic Materials?

Hyperelastic materials are characterized by their ability to undergo large deformations while maintaining the potential for complete recovery. Unlike linear elastic materials, hyperelastic materials exhibit non-linear stress-strain relationships and can experience significant shape changes without permanent deformation. Common examples include:

  • Rubber
  • Silicone
  • Biological tissues
  • Certain polymers

Steps to Model Hyperelastic Materials in Abaqus

1. Choose the Right Hyperelastic Material Model

Abaqus offers several hyperelastic material models:

  1. Mooney-Rivlin Model
    • Best for rubberlike materials
    • Captures non-linear behavior at moderate strains
    • Requires two material constants
  2. Ogden Model
    • Excellent for large deformations
    • More flexible than Mooney-Rivlin
    • Can model a wider range of material behaviors
  3. Arruda-Boyce Model
    • Microsphere-based approach
    • Good for describing rubber-like materials at large strains
    • Based on molecular network theory

2. Obtain Material Characterization Data

To accurately model a hyperelastic material, you’ll need:

  1. Experimental Data: Uniaxial, biaxial, volumetric and pure shear test results
  2. Stress-Strain Curves: Comprehensive data across different loading conditions
  3. Material Constants: Determined through curve fitting of experimental data

Tips for Data Collection:

  • Use high-precision testing equipment
  • Conduct tests at multiple strain rates
  • Cover a wide range of deformation conditions

3. Material Parameter Identification in Abaqus

Follow these steps to identify material parameters:

  1. Import Experimental Data
    • Use Abaqus Standardized Test Data (*.odb or *.txt files)
    • Ensure data is clean and well-preprocessed
  2. Material Parameter Optimization
    • Utilize Abaqus Parameter Identification capabilities
    • Minimize the difference between experimental and simulated results
    • Use least-squares or other advanced curve-fitting techniques

4. Implementing the Hyperelastic Material Model

5. Meshing and Boundary Conditions

  • Use Reduced Integration Elements: Minimize hourglassing
  • Apply Appropriate Boundary Conditions: Match experimental setup
  • Mesh Refinement: Ensure element quality for accurate results

Common Challenges and Solutions

  1. Numerical Instabilities
    • Use smaller increments
    • Apply smooth loading conditions
    • Check element formulation
  2. Material Parameter Uncertainty
    • Perform sensitivity analysis
    • Use robust parameter identification methods
    • Validate against multiple experimental datasets

Best Practices

  1. Validate Your Model: Compare simulation results with experimental data
  2. Use Multiple Testing Conditions: Uniaxial, biaxial, volumetric and planar shear tests
  3. Document Material Parameters: Maintain clear records of constants and sources

Conclusion

Modeling hyperelastic materials in Abaqus requires a systematic approach combining experimental data, material modeling expertise, and careful simulation setup. By following these guidelines, you can develop accurate and reliable computational models of complex non-linear materials.

Additional Resources

  • 1) Abaqus Theory and Reference Manuals
  • 2) ASTM Standards for Rubber Testing
  • 3) Kartik, Hyperelastic and Viscoelastic Characterization of Polymer Materials

About the Author

Kartik Srinivas, AdvanSES Laboratory K2S LLP

Keywords

Hyperelastic materials, Abaqus simulation, material modeling, non-linear materials, finite element analysis, rubber modeling, material characterization

Contact us for your material testing and FEA needs

Fatigue Testing of Rubber Materials: ASTM D430, ASTM D813 and ASTM D4482

Fatigue testing of rubber materials under dynamic tensile stretching conditions involves subjecting rubber samples to repeated elongation and relaxation cycles to evaluate their durability and performance over time.

The primary goal is to assess how rubber materials behave under cyclic loading, which can lead to fatigue failure due to the growth of micro-cracks. This can be under relaxing and non-relaxing conditions.

Rubber specimens are typically clamped at both ends and stretched repeatedly using a machine capable of applying cyclic loading or stretch. The stretching can be performed at various frequencies, amplitudes, and temperatures to simulate different service conditions. Key test parameters measured include the number of cycles to failure, the elongation at break, and the stress-strain behavior during the test. The growth of cracks and the energy required to propagate them can also be monitored.

The fatigue life of the rubber is then determined by the number of cycles it can withstand before failure. This data helps predict the material’s lifespan in real-world applications and suitable design and material compound ingredients can then be further iterated upon to achieve a higher fatigue life.

Fatigue testing is crucial for industries that use rubber components in dynamic environments, such as automotive tires, mounts, bushings, aerospace seals, gaskets and hoses etc.

ASTM D430, ASTM D813, and ASTM D4482 are the key test methods for fatigue testing of rubber materials and componds.

ASTM D430: This test method focuses on dynamic fatigue. It measures the effects of repeated distortions (such as extension, compression, or bending) on rubber materials. The test is conducted using a flexing machine in a controlled environment. It’s suitable for both pure rubber and rubber combined with other materials, like fabrics or cording.

ASTM D813: This test method is designed to measure crack growth in rubber materials. The rubber sample is pierced, clamped into a flexing machine, and subjected to a prescribed number of flexing cycles. The growth of the pierced area is observed and measured over time. It’s particularly important for testing synthetic rubber materials.

ASTM D4482: This test method evaluates extension cycling fatigue. Unlike other flex fatigue tests, ASTM D4482 is conducted on a whole sample without any cuts or punctures. It measures the rubber’s ability to withstand repeated elongation and relaxation cycles.

AdvanSES Laboratory can provide you with all the durability data for your compounds and materials. Contact us for a quick quote.

Poisson’s Ratio Testing of Polymers, Thermoplastics and Composite Materials

Poisson’s ratio: the ratio of lateral to longitudinal strain between two axial strains points is a fundamental property of the material and is imperative for accurate Finite Element Analysis (FEA) of plastic and composite materials.

ASTM D638, ISO 527 as well as ASTM D3039 establish the test conditions for tensile testing of polymers, thermoplastics, and fiber-reinforced plastics.

Advanses Laboratory can accurately provide you with the material data and results required to fully characterize your polymeric, thermoplastic and composite materials for accurate, and reliable mateial/product development and FEA simulations.

More information at https://www.advanses.com

Contact us today for a quick quote.

Poisson's Ratio Testing of Polymers, Thermoplastics and Composite Materials
Po

Unlocking the Potential of Hyperelastic Materials through Advanced Testing Techniques

Introduction: Hyperelastic materials have been gaining significant attention in recent years due to their unique properties, which make them ideal for a wide range of applications. From medical devices to aerospace engineering, these materials are revolutionizing various industries and providing new opportunities for innovation. However, testing hyperelastic materials can be challenging due to their complex behavior under different loads and conditions. In this blog post, we will explore the importance of advanced testing techniques for hyperelastic materials and how they can help unlock their full potential.

Hyperelastic Hypoelastic Viscoelastic Material Testing and FEA

Importance of Hyperelastic Materials: Hyperelastic materials are characterized by their ability to undergo large deformations without breaking or losing their shape. This unique property makes them ideal for applications where traditional materials may not perform as well. Some examples of hyperelastic materials include:

1. Shape-memory alloys (SMAs) 2. Polymeric materials 3. Metamaterials 4. Biocompatible materials

Advanced Testing Techniques for Hyperelastic Materials: To fully exploit the potential of hyperelastic materials, advanced testing techniques are necessary to evaluate their behavior under different loads and conditions. At AdvanSES laboratory some of the most common advanced testing techniques used for hyperelastic materials are:

1. Single axial Testing: This is a simple and widely used method for evaluating the mechanical properties of hyperelastic materials. The material is stretched or compressed along one axis, and the resulting stress-strain curve is recorded. Examples of unidirectional testing are Uniaxial tension test, uniaxial compression test, planar shear tests etc.

2. Multiaxial Testing: This technique involves applying loads to the material in multiple directions simultaneously. This provides a more comprehensive understanding of the material’s behavior under complex loading conditions. Examples of multiaxial testing are volumetric tests, biaxial tension tests etc.

3. Dynamic Testing: By subjecting the material to dynamic loading, such as impact or vibration, engineers can evaluate its response to sudden changes in load.

4. Fatigue Testing: Hyperelastic materials are susceptible to fatigue failure, just like any other material. Fatigue testing helps to evaluate the material’s resistance to cyclic loading and to identify potential failure points.

5. Impact and High Strain Rate Testing: Hyperelastic materials can be prone to damage or failure due to impact loading. Impact testing helps to evaluate the material’s resistance to sudden impacts and to identify potential failure points. 7. Thermal Testing: Hyperelastic materials can undergo significant changes in shape and properties due to temperature fluctuations. Thermal testing helps to evaluate the material’s thermal stability and to identify potential thermal-related failures.

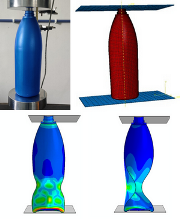
Simulation of Polymeric Material Products

Benefits of Advanced Testing Techniques for Hyperelastic Materials:

1. Improved Material Selection: By evaluating the mechanical properties of different hyperelastic materials using advanced testing techniques, engineers can select the most appropriate material for a particular application.

2. Optimized Design: Advanced testing techniques help to optimize the design of hyperelastic components by identifying their potential failure points and improving their overall performance.

3. Enhanced Manufacturing Processes: By understanding the behavior of hyperelastic materials under different loads and conditions, manufacturers can optimize their manufacturing processes to produce high-quality components with improved properties.

4. Increased Safety: Advanced testing techniques help to identify potential failure points in hyperelastic materials, which can increase safety in various industries such as aerospace, automotive, and medical devices.

5. Cost Savings: By reducing the risk of material failures through advanced testing techniques, manufacturers can save costs associated with material replacement, repair, or redesign.

Conclusion: Advanced testing techniques are essential for evaluating the behavior of hyperelastic materials under different loads and conditions. These techniques provide engineers with a better understanding of the material’s properties and help to optimize material selection, design, and manufacturing processes. By adopting advanced testing techniques, industries can improve safety, reduce costs, and enhance the overall performance of hyperelastic materials in various applications.